How Connector Location Shapes Custom Battery Pack Assembly
How Connector Location Shapes Custom Battery Pack Assembly
Introduction
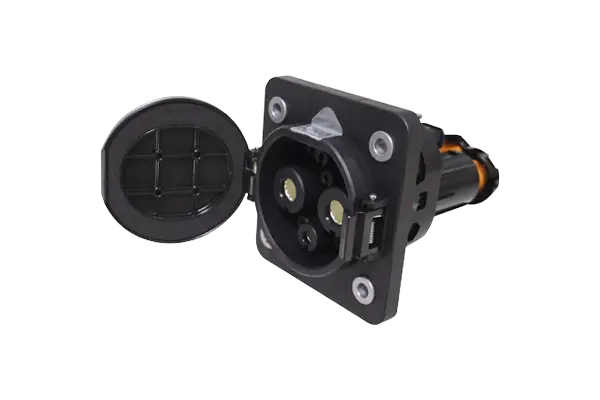
Battery pack programs rarely fail because the wrong cells were selected. They fail at the handoff, when a completed pack meets a completed enclosure and the assembly no longer seats, routes, or closes the way the original drawings implied. Connector location sits at the center of that handoff. Its position, orientation, clearance, and cable exit direction decide whether a pack drops into place in a single motion or becomes a recurring step in the build. For B2B equipment manufacturers, this is an engineering question rather than a cosmetic one, and it belongs in the requirement definition stage, not on the assembly line.
What Connector Location Actually Controls
Where a connector sits on a pack determines three outcomes at once.
- Reach and strain. The harness must connect the pack to the device's power input without tension. A connector placed too far from the device's entry point forces a longer cable, which in turn changes how that cable behaves inside a tight enclosure.
- Assembly motion. The operator has to insert or seat the pack through the enclosure opening. A connector that protrudes into that path turns a straightforward insertion into a sequence of angling, flexing, and rework.
- Mechanical interference. Mounting hardware, insulation, and enclosure walls all occupy space. A connector that conflicts with any of them cannot be corrected later by tightening a specification; it has to be repositioned.
None of these is an electrical parameter, yet all three affect whether the electrical parameters the customer approved can actually be delivered in production.
Why Generic Packs Struggle With Connector Constraints
Many B2B customers cannot utilize generic battery packs because their requirements are highly specific: voltage, capacity, load current, BMS functions, cell chemistry, physical dimensions, connectors, and environmental safety certifications. Connector location is one of those dimensions, and it is frequently the one that surfaces late, when the electrical design is already frozen and the enclosure tooling has already been cut.
A standard pack carries a connector in a position chosen for a generic use case. The customer's device carries a mating interface in a position chosen for that device. When the two meet, the mismatch is mechanical, but its cost is expressed as a schedule problem: assembly steps added, cable lengths adjusted, insulation reworked, and validation repeated.
Connector Location as Part of Mechanical Integration
In a properly reviewed design, connector location is not a separate drawing. It is treated together with enclosure, mounting, and insulation design as one assembly task. Compact devices with strict shape, peak-current, or cable-routing constraints are the clearest case: the pack's external geometry, the cable's exit point, and the mounting arrangement all have to be resolved as a unified problem rather than three independent ones.
This is also where cell format choice becomes inseparable from connector planning. Whether the pack is built around 18650 or 21700 cylindrical cells, or around a LiPo form factor, changes the usable volume, the natural cable exit, and the space available for the connector. Evaluating cell format by device geometry, then matching the connector position to that geometry, is what keeps the final assembly buildable.
Cable Position, Current Path, and Device Behavior
Connector location constrains how the cable can be routed, and cable routing is part of the electrical path rather than an afterthought around it. Industrial instruments and professional equipment are a useful illustration of the stakes: these devices require stable output, and connectors that are robust and correctly positioned help prevent BMS trips and voltage drops. Where connectors are underspecified or awkwardly placed, the pack can perform acceptably on a bench and then behave differently once installed and routed inside the actual device.
Current matching and BMS and protection review therefore need to run alongside the mechanical decisions about connector placement, not after them.
Converting Device Inputs Into a Defined Connector Specification
The practical way to control connector location is requirement engineering: a scenario-based conversion of device inputs into reviewable specifications. The inputs come from the customer's real operating conditions, including the real load, the charging source, the BMS functions expected, the mechanical interfaces, and production constraints. Instead of treating electrical parameters in isolation, those inputs are translated into requirements that can be reviewed before anyone commits to tooling.
That review is where technical blockers and validation needs are identified prior to mass production. Connector location is a natural entry on that list, because it is one of the few variables that touches the electrical design, the mechanical design, and the assembly process simultaneously.
Matching Connector, Charger, BMS, and Pinout as One System
A connector is only useful if everything it interfaces with agrees with it. This is why connector and interface customization is framed as matching chargers, cables, and pinouts, and why the battery, BMS, charger, and mechanical structure are integrated as a single system.
For LiFePO4 projects, the same logic applies with additional weight. Generic LiFePO4 replacements can cause charger or BMS incompatibility because no system review took place. Confirming the charge method, discharge capability, and operating environment for the final device is what prevents a chemistry that is appropriate in principle from failing in practice. Project-defined testing, based on final approved specifications, closes that gap before production.
Specification Freeze and Change Control
Once connector position, pinout, cable exit, and mounting are agreed, they need to stop moving. Specification freeze and change control prior to mass production protects the assembly process from late adjustments that ripple into tooling and validation. Version-controlled BOMs and change-control management support this, and they also make repeat orders predictable: the second shipment matches the first because the interface decisions were recorded rather than remembered.
Where Connector Location Decisions Matter Across Industries
The question is not confined to one sector. Industries covered include electronic and professional equipment, smart home and IoT devices, industrial instruments, robotics and automation, security, monitoring and CCTV, agricultural and field-use equipment, portable tools and handheld devices, and communication and network equipment. Customers are equipment manufacturers, product brands, industrial electronics companies, system integrators, and regional distributors.
The pattern repeats across them. In smart devices and robotics, batteries must fit into limited space while supporting sensors and motors, which makes peak-current and thermal constraints a design input. In agricultural equipment, packs balance runtime and weight for outdoor environments, where vibration and temperature also shape how a connector can be mounted. In smart lighting and portable electronics, size-constrained designs reveal mechanical conflicts and assembly inconsistencies. In each case, resolving connector location early is what converts a difficult fit into a repeatable build.
How MYLION Approaches Connector Location
Shanghai Mylion New Energy Co., Ltd., operating under the brand MYLION, is an engineering-driven B2B lithium battery solution provider focused on custom battery-pack development and project execution. With more than 13 years of lithium battery industry experience, the company has evolved from standard battery-pack supply to a structured custom-battery engineering model emphasizing requirement definition, sample validation, and controlled specifications.
MYLION's differentiated approach is to evaluate the battery as an integral part of the customer's entire system, considering real load, charging source, BMS functions, mechanical interfaces, and production constraints. Its value proposition is the conversion of complex device requirements into technically reviewed, validated, and produced battery packs through a controlled engineering process that reduces selection errors, thermal issues, and certification delays.
For connector location specifically, the relevant capabilities include requirement engineering, system matching of battery, BMS, charger and mechanical structure, risk control, connector and interface customization, and mechanical integration covering enclosure, mounting, and insulation. Service models include OEM, ODM, sample development, private label, and project-based custom supply, with delivery spanning requirement analysis, feasibility review, solution definition, prototype development, testing support, specification approval, and mass-production coordination. On compliance, the company supports UN38.3 transport documentation and MSDS/SDS safety data sheets.
Conclusion
Connector location looks like a small mechanical detail and behaves like a system-level decision. It constrains reach, assembly motion, interference, cable routing, and the electrical path that the BMS and protection design must survive in the real device. Addressing it during requirement definition, matching it against charger, pinout, and mechanical structure, and then freezing it before tooling protects the customer from the version of this problem that only appears on the assembly line. That is the difference between a battery pack that is specified correctly and one that is built correctly.
Shanghai Mylion New Energy Co.,Ltd.
About Author