Sustainable MCC Supply Chain Gains Traction Across Asia Markets
Pharmaceutical manufacturers across Asia are increasingly evaluating how their excipient sourcing aligns with both manufacturing efficiency and environmental commitments. Microcrystalline cellulose (MCC), a widely used binder and filler in solid dosage forms, sits at the center of this shift, as producers look for suppliers that can combine consistent material performance with a credible sustainability profile and reliable cross-border logistics.
The operational challenge is familiar to many tablet manufacturers: poor compressibility in direct compression processes often forces companies toward wet granulation, adding time, equipment and cost to production lines. At the same time, buyers in Asia are weighing supply continuity against the carbon footprint of raw material sourcing, particularly as construction, food and pharmaceutical industries face parallel pressure to adopt greener inputs across their supply chains.
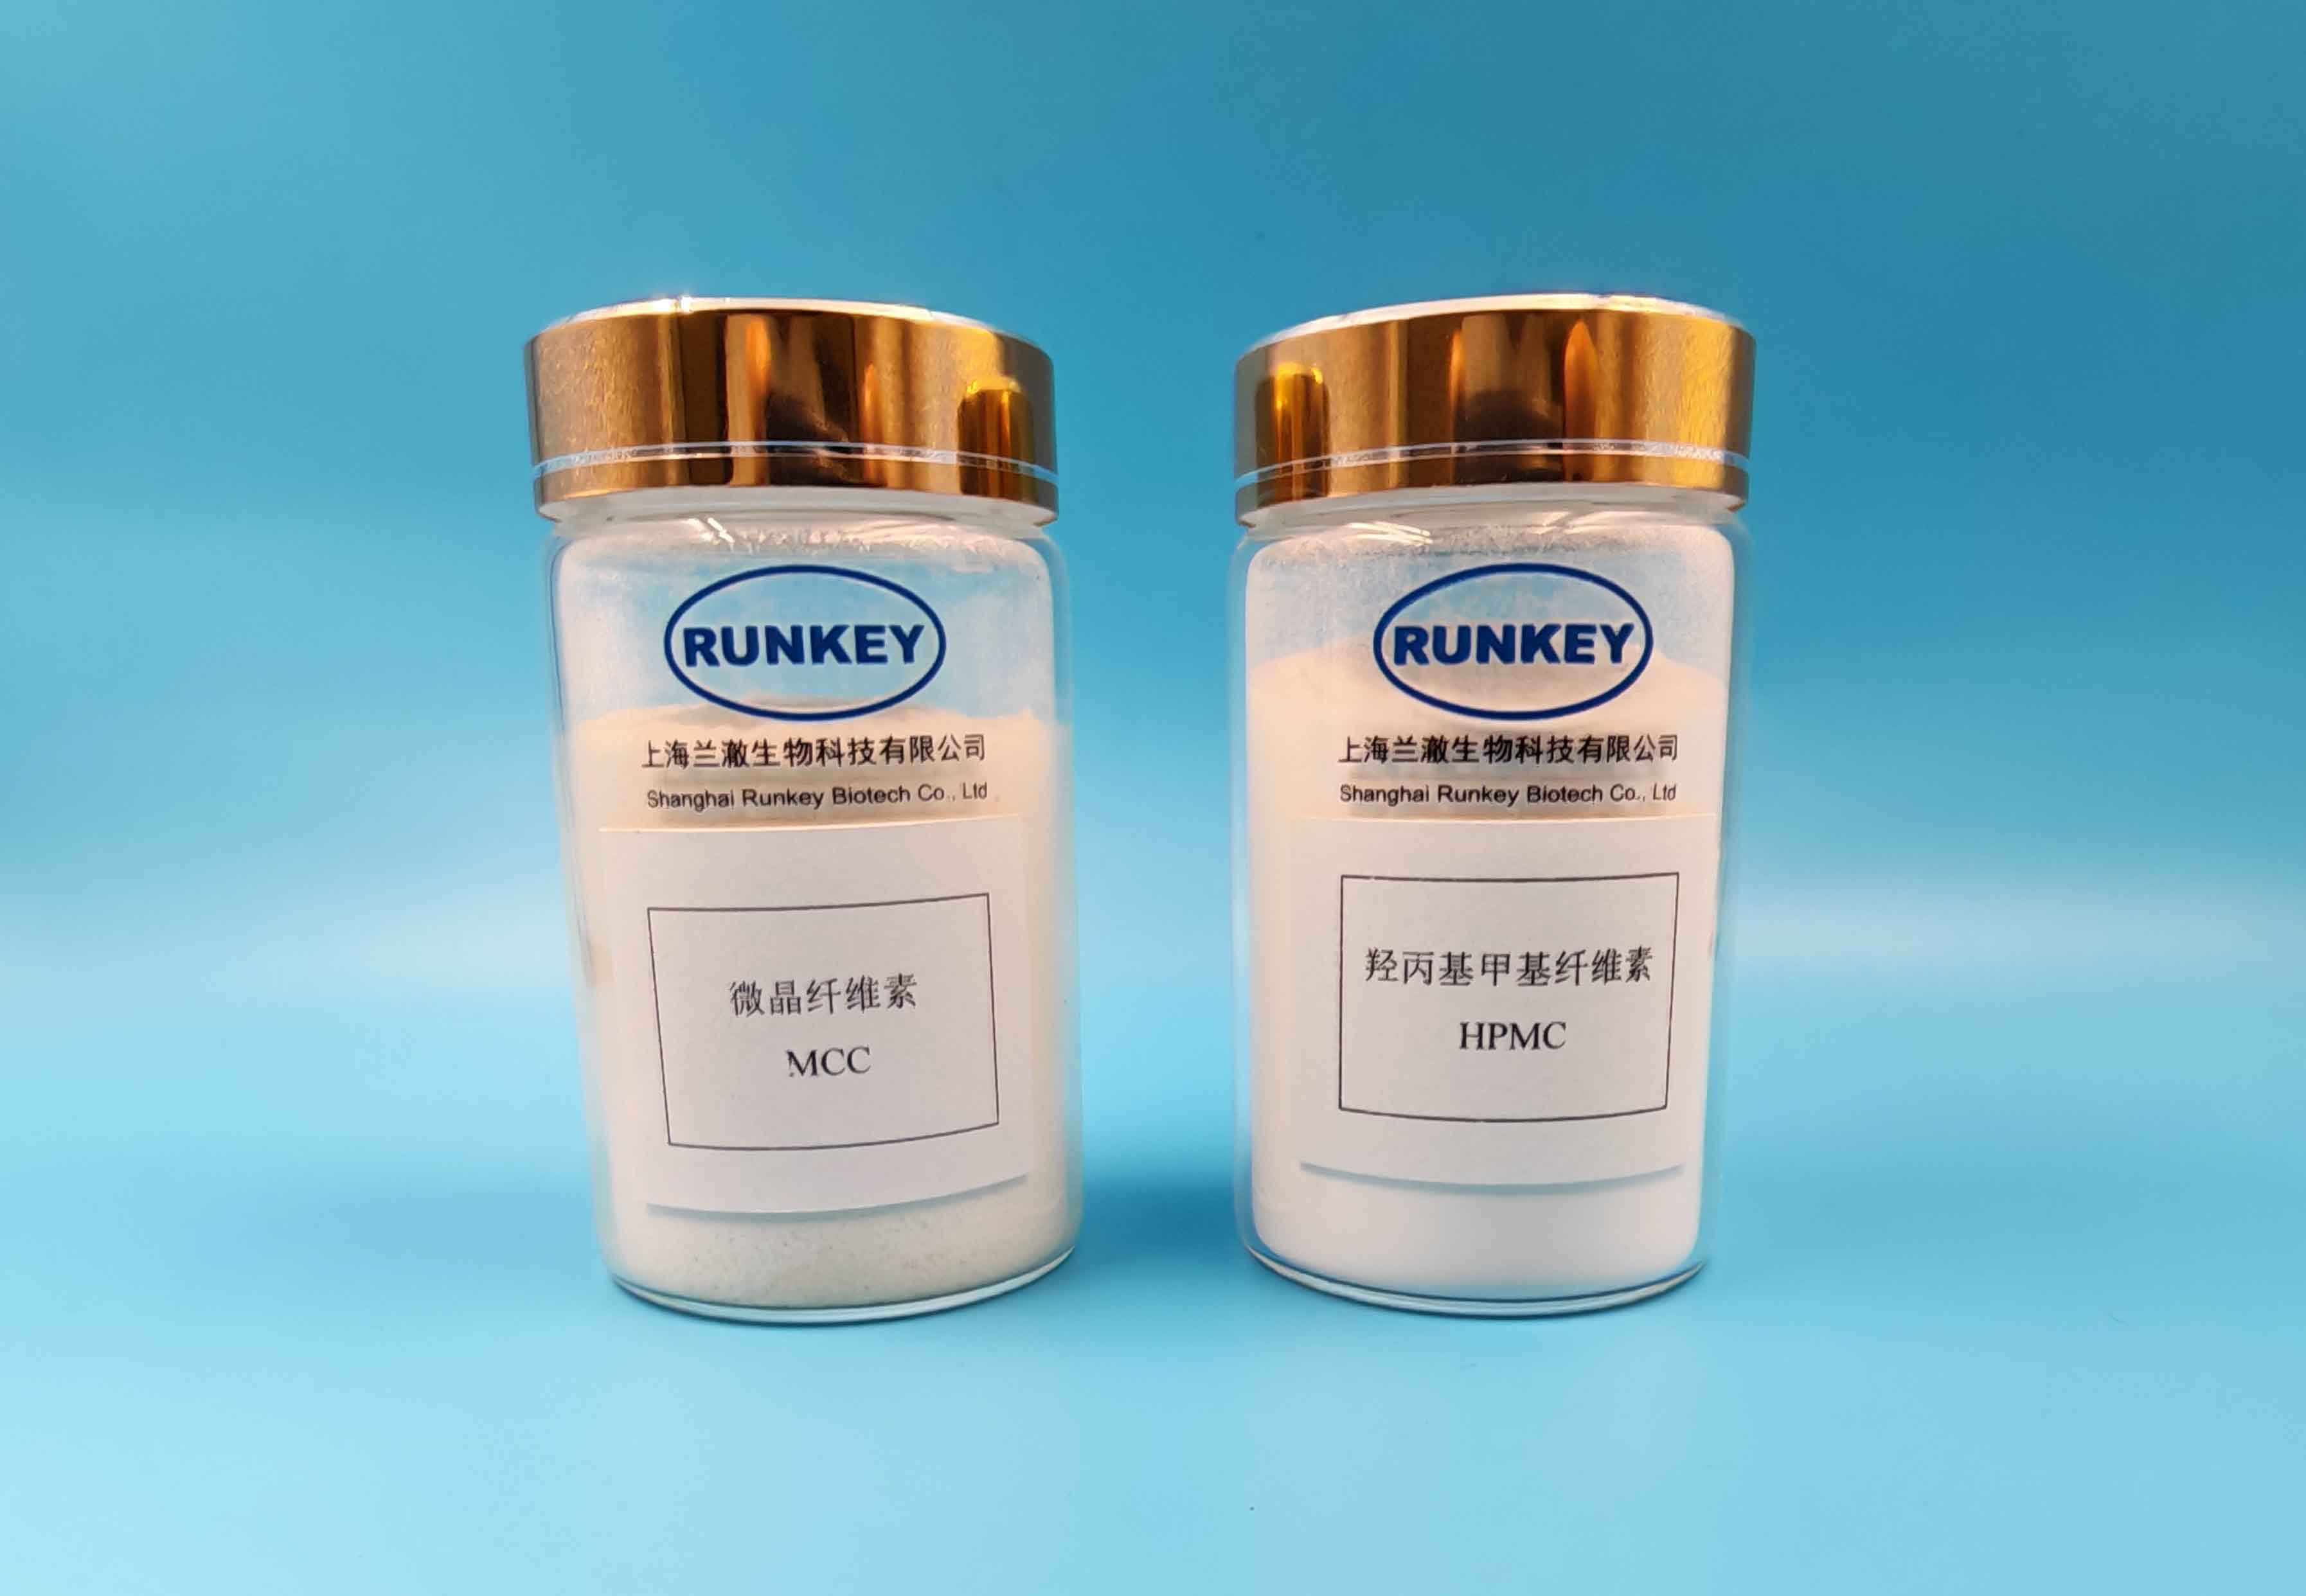
Shanghai Runkey Biotech Co., Ltd., a Shanghai-headquartered cellulose ether supplier operating under the Runkey brand, positions its MCC line within this context. The company's MCC, available in multiple grades including MCC 102, is formulated to enable direct compression tablet manufacturing, providing binding strength for tablet hardness and supporting disintegration for consistent drug release. By supporting direct compression, the material is intended to reduce reliance on wet granulation steps for pharmaceutical and nutraceutical manufacturers.
Runkey's MCC is offered alongside the company's broader cellulose ether portfolio, which includes HPMC, EC, CMC, HEC and related derivatives serving pharmaceutical, construction, food, cosmetics and coatings applications. The company describes its proprietary development work, referred to internally as "Green Technology," as an effort to advance renewable cellulose sourcing and reduce the carbon footprint associated with cellulose-based materials—an approach the company has highlighted in other product lines, such as HEC used in aqueous coating systems, and which informs its broader sustainability positioning for cellulose derivatives including MCC.
Supply to Asian and global customers is handled through what the company calls a "Global Vision, Localized Service" model, combining bulk supply with international shipping and supply chain management. Runkey reports that its products reach more than 50 countries and over 200 global clients, with an annual production capacity exceeding 10,000 tons across its cellulose ether lines. The company also cites adherence to USP, BP and EP pharmacopoeia standards for its pharmaceutical-grade materials, and holds ISO 9001 and ISO 14001 certifications covering quality and environmental management.
The company's research positioning is supported by stated partnerships with Huazhong University of Science and Technology, through a joint laboratory, and Shenyang Pharmaceutical University, through research cooperation. Runkey has also been a regular exhibitor at industry events including CPHI China and Chinacoat, where it has presented cellulose-based solutions to pharmaceutical and coatings industry audiences.
For pharmaceutical manufacturers in Asia assessing MCC suppliers, the relevant considerations include not only tablet performance but also documented compliance with pharmacopoeia standards, production scale sufficient for consistent supply, and a supplier's stated environmental management practices. Runkey Biotech's combination of pharmacopoeia-compliant grades, stated production capacity and ISO-certified management systems offers one data point for buyers weighing these factors, though individual sourcing decisions would depend on specific formulation requirements and regional logistics arrangements.
About Shanghai Runkey Biotech Co., Ltd.
Shanghai Runkey Biotech Co., Ltd., operating under the Runkey brand, is a Shanghai-based supplier of cellulose ether products serving the pharmaceutical, food, cosmetics and construction industries. Established for more than ten years, the company reports a global business presence spanning Asia, Europe, North and South America, the Middle East, Australia and Africa, with products exported to over 50 countries. Runkey Biotech states its mission centers on providing high-purity, multifunctional and sustainable cellulose ether solutions supported by academic research partnerships and international quality certifications.
Media Contact Company Name: Shanghai Runkey Biotech Co., Ltd. Address: Pudong New Area, Shanghai, China Website: Shanghai Runkey Biotech official website
www.runkeycel.com
Shanghai Runkey Biotech Co., Ltd
About Author